Material Handling Solutions
SolutionsFMCG

FMCG and food production.

Fast-moving consumer goods run on volume and dates. Product arrives, moves through chill or ambient storage, gets picked and dispatched, often within days, sometimes hours. The forklift fleet is either keeping up or it's the reason you're not.

MHS supplies material handling equipment to food producers, beverage manufacturers and FMCG distributors across New Zealand, including operations running chilled, frozen and ambient environments side by side.

What do FMCG operations need from a forklift?
1
Machines that survive the cold.
Chillers and freezers punish standard equipment. Condensation, seal failure and hydraulic performance in sub-zero temperatures are all real problems, and battery capacity drops noticeably in the cold. Cold store models are built for it; standard machines adapted for it generally aren't.
2
A charging strategy that fits the shift pattern.
FMCG runs long hours, often around the clock. Lead-acid needs downtime and swap infrastructure. Lithium can be opportunity-charged during breaks, which is why high-utilisation food and beverage sites are the clearest case for it in New Zealand.
3
Food-grade compliance.
Non-marking tyres, food-safe lubricants and washdown-tolerant components are requirements on many sites, not preferences. Worth confirming before a machine arrives rather than after an audit.
4
Speed without damage.
High throughput and fast pick rates raise the odds of racking strikes and product damage. Operator aids such as camera systems, height selectors and speed limiting by zone pay for themselves quickly where stock value per pallet is high.
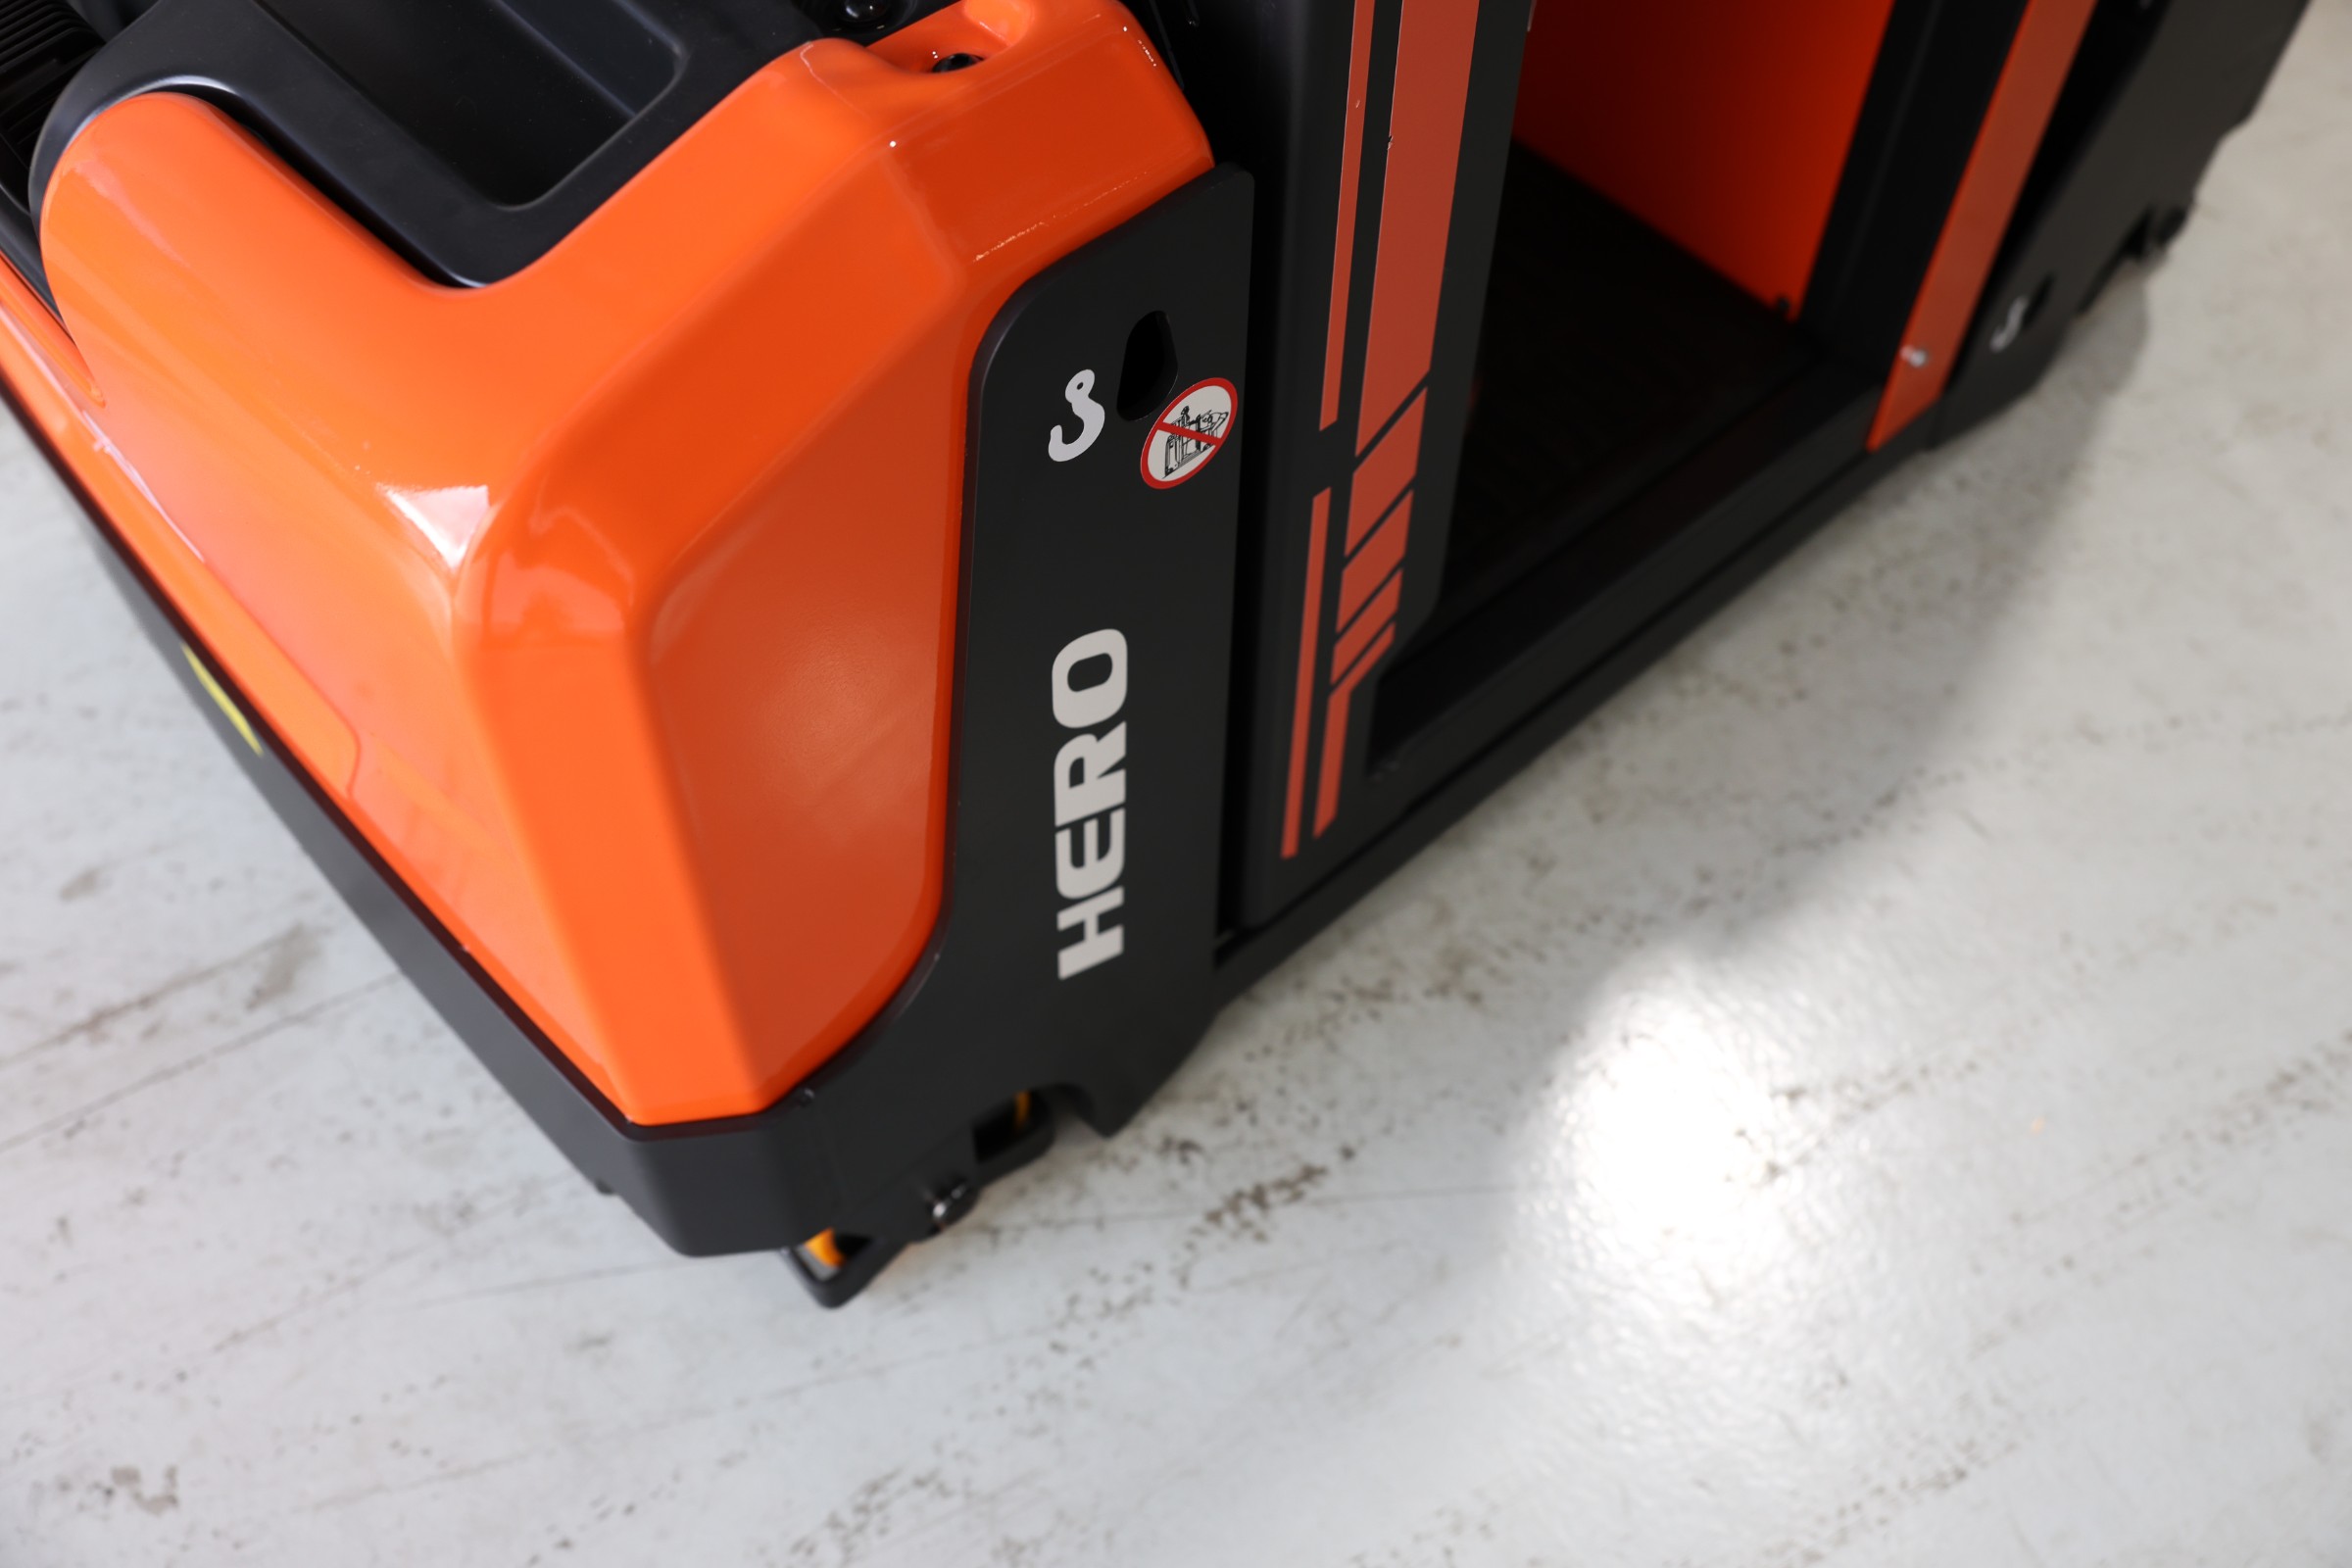
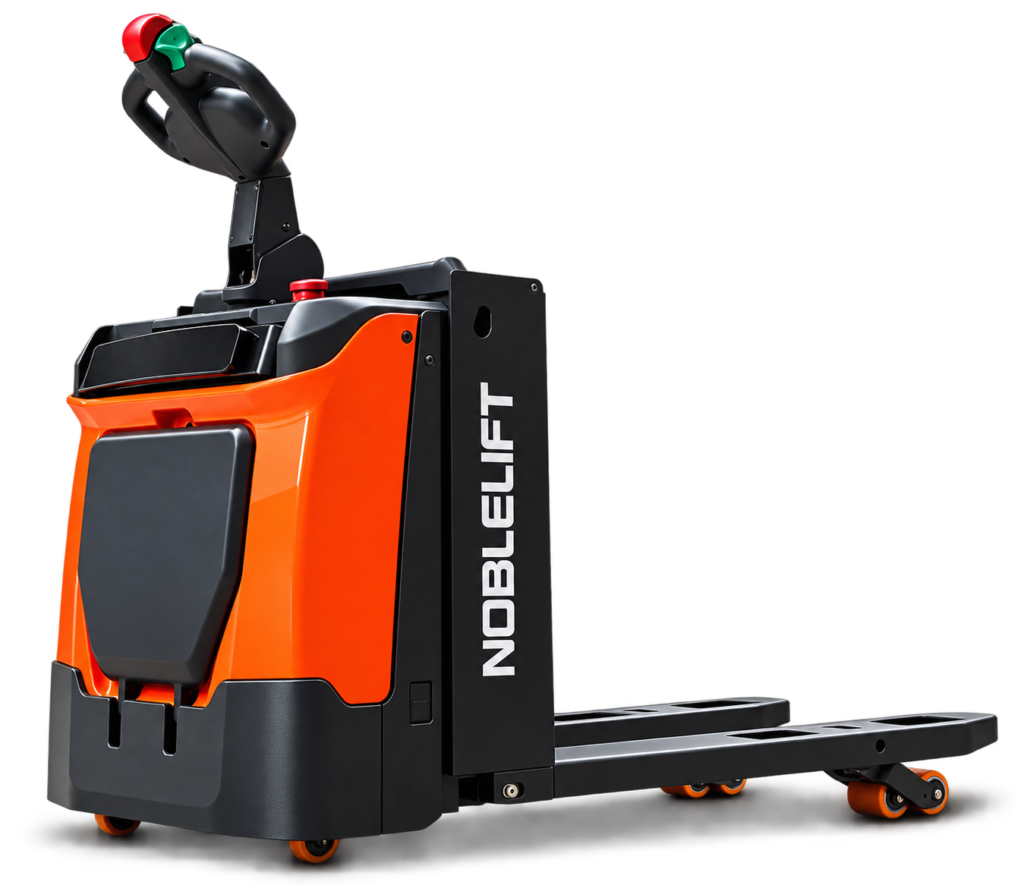
Noblelift HERO order picker
How we specify FMCG equipment
Temperature zones the machine will work in, and how often it crosses between themShift pattern and charging windowsFood-safety and site compliance requirementsPick rates and peak throughputRacking layout and aisle widthsProduct value and damage risk per pallet

Forklifts for FMCG

View all products
Supporting FMCG businesses across New Zealand

MHS supplies forklifts and material handling equipment to food producers and processors, beverage manufacturers, dairy and protein operations, FMCG distributors and cold storage facilities.

These sites can't afford a machine sitting idle waiting for a part. Every machine we supply is backed by MHS parts and technicians, with scheduled servicing and breakdown support from Auckland and Christchurch.

Talk to the MHS team
Contact an MHS specialist.

Choosing the right forklift is an important investment in your operation. Our team is ready to help you identify the best equipment solution for your warehouse, yard or distribution centre.

What do you need?*
We'll respond within 1 business day. Your details are safe with us.